Ti-6242 (Ti-6Al-2Sn-4Zr-2Mo) Engine & Turbine CNC Parts
High-temperature near-alpha alloy engineered for aerospace turbine blades, impellers, and exhaust components operating up to 540°C.
View SpecificationsEngineered for extreme environments in aerospace, defense, subsea energy, and surgical medical devices. Manufactured from Grade 5 (Ti-6Al-4V), Grade 2, Ti-6242, and Grade 23 ELI using multi-axis 5-axis milling, Swiss turning, and ultra-tight tolerance EDM processes (±0.005 mm).
In modern precision manufacturing, Titanium CNC Machined Parts represent the pinnacle of structural integrity, corrosion immunity, and elevated strength-to-weight performance. However, procuring custom titanium machined components requires a deep understanding of metal metallurgy and cutter-workpiece interaction physics. Unlike standard carbon steel or aluminum alloys, titanium alloys possess unique mechanical properties that complicate subtractive CNC machining operations:
Titanium’s thermal conductivity is exceptionally low (~6.7 W/m·K for Grade 5, vs 160 W/m·K for 6061 Aluminum). Over 80% of heat generated during cutting transfers directly into the cutter edge rather than dissipating via chips, triggering thermal micro-cracking and rapid tool wear.
With an elastic modulus roughly half that of stainless steel (110 GPa for Ti-6Al-4V vs 200 GPa for 316L), thin-walled titanium components exhibit significant springback under cutting tool forces, requiring specialized multi-axis vibration dampening fixtures.
At temperatures exceeding 500°C, titanium reacts chemically with cutting tool materials (galling and chip welding), necessitating high-pressure coolant (HPC) delivery systems (>70 bar) directly targeted at the shear zone.
At Almerca Titanium Industry Co., Ltd., we utilize state-of-the-art 5-axis CNC machining centers (DMG MORI, Mazak) and Swiss automatic lathes optimized specifically for titanium alloys. Our cutting geometry, high-pressure cryogenic and oil-mist cooling techniques, and custom carbide tool coatings (AlTiN, TiAlN) eliminate work hardening and guarantee ultra-repeatable tolerances down to ±0.005 mm.
Global buyers frequently encounter lead time inflation due to raw material porosity or tool failure during milling. Almerca Titanium Industry Co., Ltd. controls the complete supply chain: from vacuum arc remelting (VAR) titanium ingot forging down to final 5-axis CNC finishing. Every titanium batch undergoes 100% Ultrasonic Testing (UT) prior to machining to eliminate internal voids and inclusion flaws.
We manufacture custom precision components based on customer CAD models (STEP, IGES, SolidWorks) and detailed engineering drawings across a comprehensive range of commercially pure (CP) titanium grades and high-strength titanium alloys:
High-temperature near-alpha alloy engineered for aerospace turbine blades, impellers, and exhaust components operating up to 540°C.
View Specifications
The workhorse aerospace titanium alloy. Delivers yield strength >880 MPa with superior fatigue fracture toughness for structural brackets and housings.
View Specifications
Precision-turned Grade 5 and Grade 2 custom bolts, studs, sleeves, and subsea connectors featuring rolled threads for maximum fatigue life.
View Fastener Range
Deep-hole drilled and 5-axis milled Grade 2 / Grade 12 manifold blocks engineered to withstand 10,000+ PSI subsea hydrostatic pressures.
View Flange & Block OptionsSelecting the optimal titanium alloy grade directly impacts component weight, chemical resistance, surface fatigue life, and total CNC manufacturing cost. The following engineering matrix outlines the technical parameters across standard titanium alloys processed by Almerca Titanium Industry Co., Ltd.:
| Titanium Alloy Grade | Standard Specs | Tensile Strength (MPa) | Yield Strength (MPa) | Machinability Index (%) | Primary Industrial Application |
|---|---|---|---|---|---|
| CP Grade 2 | ASTM B348 / UNS R50400 | ≥ 345 | ≥ 275 | 45% (Easiest CP) | Chemical processing valves, marine heat exchangers, desox piping |
| Ti-6Al-4V (Grade 5) | ASTM B348 / AMS 4928 | ≥ 895 | ≥ 828 | 22% (Moderate) | Aerospace airframes, engine brackets, racing automotive, defense |
| Ti-6Al-4V ELI (Grade 23) | ASTM F136 / ISO 5832-3 | ≥ 860 | ≥ 795 | 25% (High Ductility) | Surgical orthopedic implants, bone screws, medical device housings |
| Ti-6242 (Ti-6242S) | AMS 4919 / UNS R54620 | ≥ 1010 | ≥ 930 | 18% (Challenging) | High-temp jet engine compressor disks, motorsport exhaust valves |
| Grade 7 (Ti-0.2Pd) | ASTM B348 / UNS R52400 | ≥ 345 | ≥ 275 | 43% (CP Palladium) | Extreme reducing acid media, marine chlor-alkali cell components |
| Grade 12 (Ti-0.3Mo-0.8Ni) | ASTM B348 / UNS R53400 | ≥ 483 | ≥ 345 | 35% (High Strength) | Elevated temperature chemical process equipment, subsea manifolds |
As global supply chains demand lower carbon footprints, reduced buy-to-fly ratios, and hyper-precise component geometries, the procurement paradigm for titanium CNC machined parts is undergoing significant technological shifts:
Traditional titanium machining often yields a wasteful 90% buy-to-fly ratio (scrap chip mass). Modern procurement increasingly mandates Near-Net-Shape (NNS) Direct Energy Deposition (DED) or Selective Laser Melting (SLM) 3D printing combined with 5-axis finish CNC milling. This hybrid approach reduces material waste by up to 65% and cuts raw material lead times from 16 weeks to 3 weeks.
Artificial Intelligence algorithms embedded in 5-axis CNC controllers now monitor spindle vibration spectra and motor torque in real-time. By dynamically adjusting feed rates (IPT) to prevent harmonic chatter, AI-driven adaptive pathing extends carbide tool life by 40% and guarantees flawless surface micro-finishes without manual polishing intervention.
With ESG compliance becoming mandatory for aerospace prime contractors, Almerca Titanium Industry Co., Ltd. utilizes segregated chip reclamation protocols. 100% of clean titanium chips produced during CNC milling are degreased, briquetted, and vacuum melted back into secondary industrial ingot feedstock, achieving full circularity.
The rapid expansion of robotic surgical instruments and bio-absorbable cardiac monitors requires micro-machined titanium parts with feature dimensions under 0.5 mm and surface finishes under Ra 0.2 µm. High-RPM Swiss automatic turning lathes featuring live tooling allow single-setup production of intricate medical titanium screws and pins.
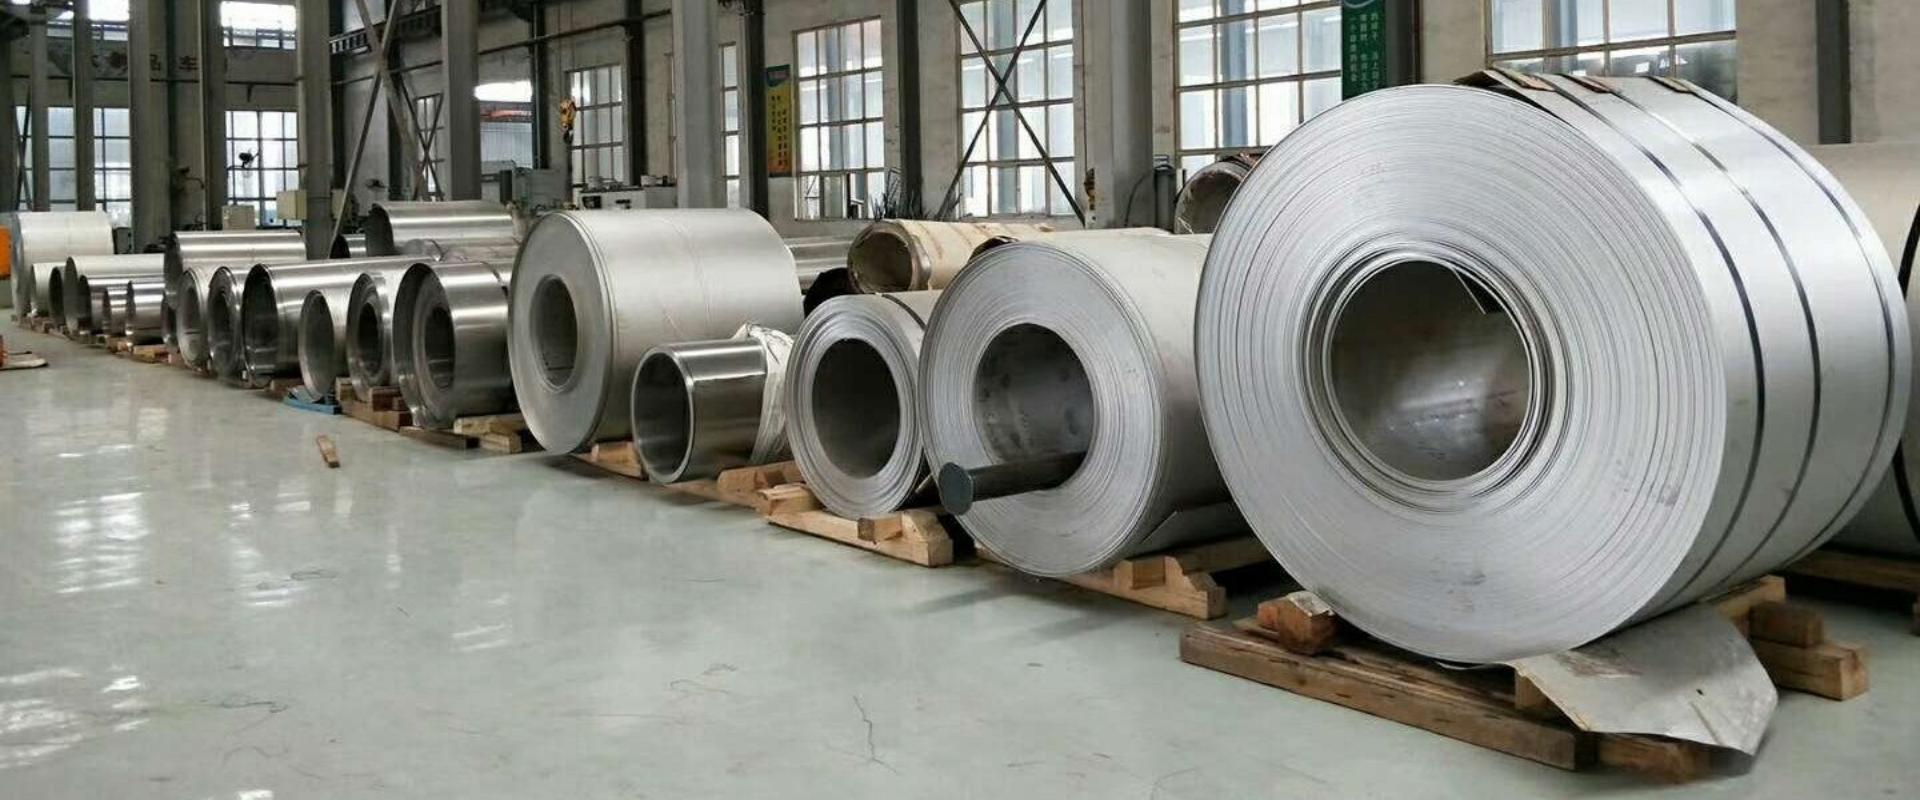
Headquartered in Shaanxi Province, China—the world-renowned hub of titanium metallurgy—Almerca Titanium Industry Co., Ltd. operates over 60,000 square meters of specialized manufacturing space equipped with over 100 advanced machining centers:
Below are technical answers to common queries submitted by global procurement managers, design engineers, and quality assurance directors when sourcing custom Titanium CNC Machined Parts:
With over 14 years of specialized titanium manufacturing mastery, certified AS9100D quality systems, and direct mill supply, Almerca Titanium Industry Co., Ltd. is your trusted global partner for high-precision Titanium CNC Machined Parts.